Innovations in High-Strength Textiles: From Industrial Applications to Specialized Accessories
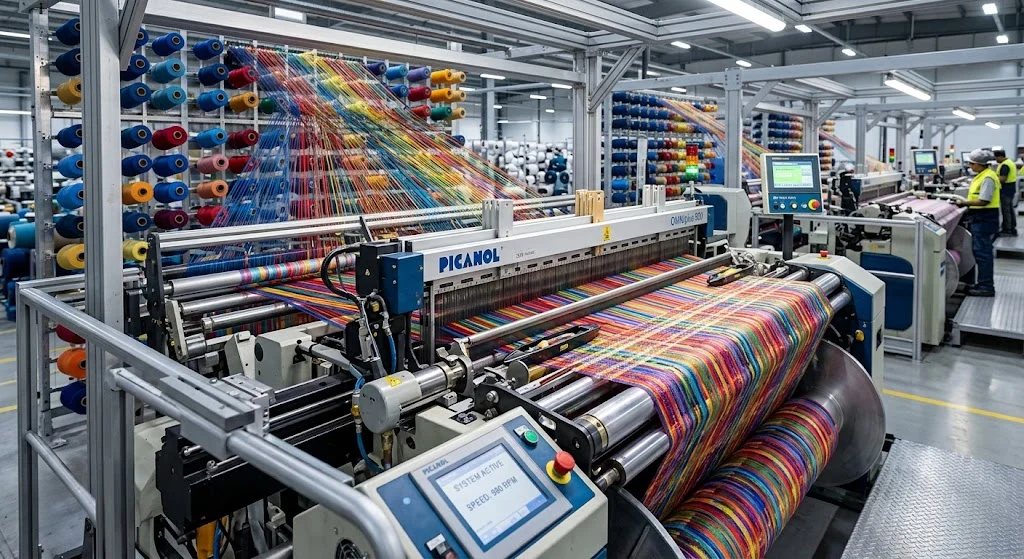 The global textile industry is undergoing a remarkable shift. Today, fabric manufacturing extends far beyond basic apparel and home decor. The current focus is heavily centered on functional, high-tenacity, and ergonomic materials designed to endure heavy usage while offering optimal user comfort.
1. High-Tenacity Fibers and Webbing Technologies
High tensile strength and wear resistance are paramount for various specialized industries, ranging from outdoor gear to medical and custom accessories. Using high-density polyamide, nylon, and polyester fibers allows manufacturers to produce specialized webbing and straps with enhanced structural integrity.
These engineered fabrics achieve a critical balance between structural firmness and tactile softness. For example, in the production of specialized equipment and adult recreational accessories, such as Bondage Toys, secure hold and body safety are essential. Textile innovations make it possible to deliver high load-bearing capacity without causing skin friction or discomfort.
2. Functional Coatings and Smart Fabrics
Beyond mechanical strength, modern textile engineering integrates advanced chemical and physical treatments to enhance performance. Modern material enhancements include:
- Water-Repellent & Breathable Membranes: Provide environmental protection while maintaining natural airflow.
- Antimicrobial Treatments: Prevent odor retention and bacterial growth over long-term use.
- Thermal Regulation: Fibers engineered to store and release heat based on ambient body temperatures.
3. Sustainability and Eco-Friendly Manufacturing
Eco-conscious production processes have become an industry standard. Leading manufacturers are adopting recycled synthetic yarns, organic cotton, and water-efficient dyeing methods. Material durability plays a vital role in sustainability: the longer a fabric lasts under tension, the lower its overall environmental footprint.
Conclusion
Technological progress in textile manufacturing opens new possibilities across diverse markets. Combining durability, safety, and ergonomics ensures that modern fabrics deliver top performance—whether for heavy-duty industrial applications or specialized personal products.
Share this article
Related Posts
Latest Posts


